Stencils Play in SMT Assembly
The world of electronics is constantly evolving as manufacturers push the limits of innovation. This means smaller and more intricate components that must be assembled with precision to ensure high quality, reliable performance. Surface mount technology (SMT) is one of the most advanced methods of assembling printed circuit boards (PCBs). SMT assembly requires specialized equipment and highly trained staff to ensure accurate component placement and reflow soldering.
The role that stencils play in smt assembly is critical, especially with the proliferation of fine-pitch technologies and miniaturized components. The right stencils are necessary to ensure the proper amount of paste is applied, resulting in an accurate placement and a successful SMT assembly. The type of stencil used depends on the production process and PCB design. There are five different types of stencils available, each suited for various production processes and applications. The type of stencil material and fabrication technique are also important factors.
In order to maximize a stencil’s performance, it is important to understand the basic principles that determine how the apertures on the stencil are formed and how they influence paste deposition. Apertures are the openings through which the paste is deposited on the PCB. The size, shape and positioning of the apertures in a stencil will directly affect how well a stencil prints, and ultimately, the quality of the finished PCB.
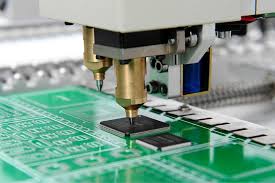
The Role That Stencils Play in SMT Assembly
For example, if a stencil has oversized apertures, the excess paste will cause uneven deposits that can lead to shorted connections or even a complete failure of the PCB. This can be prevented by selecting a stencil with apertures that are proportional to the PCB’s pad size. In addition, the stencil’s thickness is a key factor in determining the quantity of paste that will be deposited. Choosing the appropriate thickness will minimize the risk of overflow and underfill and will help ensure that each pad has an adequate amount of solder.
Another consideration is how the apertures are positioned with respect to the squeegee blade. Apertures that are too close to the squeegee blade will cause excessive squeegee pressure, which can damage both the stencil and the PCB. It is recommended that the apertures be positioned far enough away from the squeegee blade to avoid this issue.
The final key factor that determines how a stencil performs is the aperture’s geometry and the amount of force that is applied to the squeegee blade. There are a number of industry standards that describe how to best match an aperture’s geometry to the squeegee-blade. For the optimum performance, an aperture’s aspect ratio should be greater than 1.5.
The best way to achieve this is by using a high-quality stencil that is made from durable materials. Stainless steel is a popular choice because it offers durability and dimensional stability, but it can be expensive. Laser-cut polyimide is a cost-effective alternative that has excellent dimensional stability and stencil life. The use of registration marks known as fiducial marks on both the stencil and the PCB will also help to guarantee proper alignment.